Marine · featured
ERNiCu-7 for seawater strainer bodies
Weld toe corrosion traced to a nickel-chromium filler used as a substitute; ERNiCu-7 restored the matching corrosion behaviour.
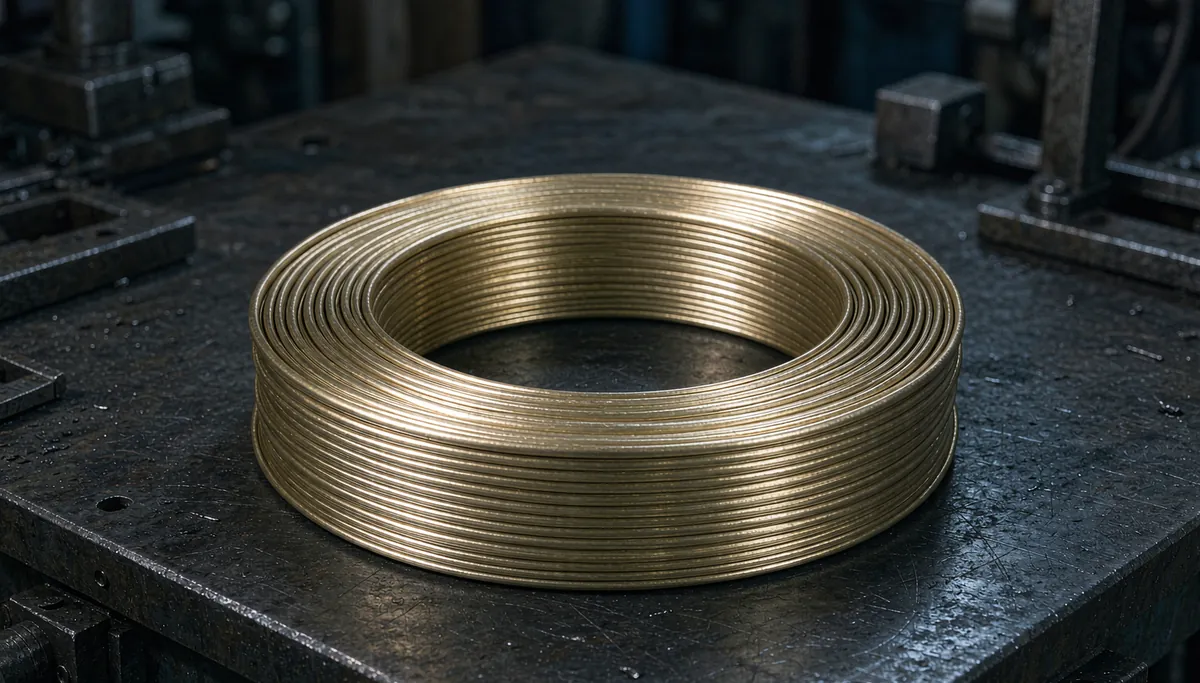
ERNiCu-7 in TIG rods and MIG spools, matched to Monel 400 and K500. Marine and chemical service where the weld has to corrode at the same rate as the parent metal — not faster.
Nickel-copper alloys depend on a continuous nickel-copper matrix for their seawater resistance. Substituting a nickel-chromium filler leaves a weld that is cathodic to the parent metal, and the parent corrodes preferentially at the toe of the weld.
ERNiCu-7 is titanium-stabilised to control porosity, which is the other common problem in Monel welding. We supply it with the deposit chemistry per batch and a reminder on the certificate: low heat input, clean joint, no preheat.
The filler is fixed by the base metal family; the variables are heat input and cleanliness.
Seawater and chemical service where the weld must match parent corrosion.
Welded in the annealed condition, then aged; ERNiCu-7 matches the matrix.
Nickel-copper to carbon steel transitions in marine systems.
Used for repair welds where a machinable, corrosion-resistant deposit is needed.
TIG for root passes and repair, MIG for production and cladding.
1 m lengths in sealed tubes; the surface stays clean until the arc starts.
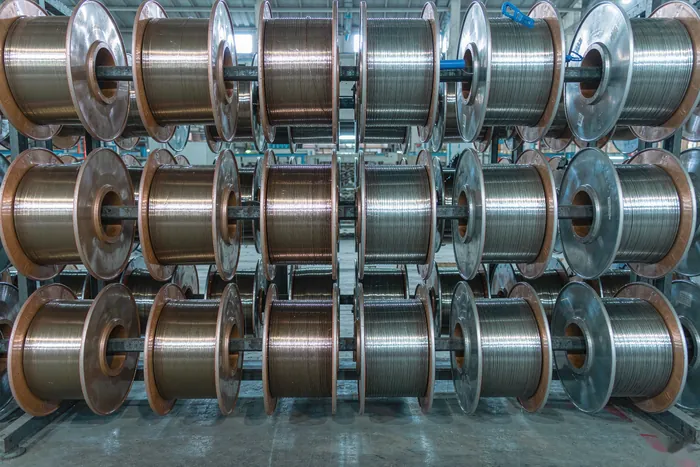
Layer wound for consistent feeding on orbital and robotic equipment.
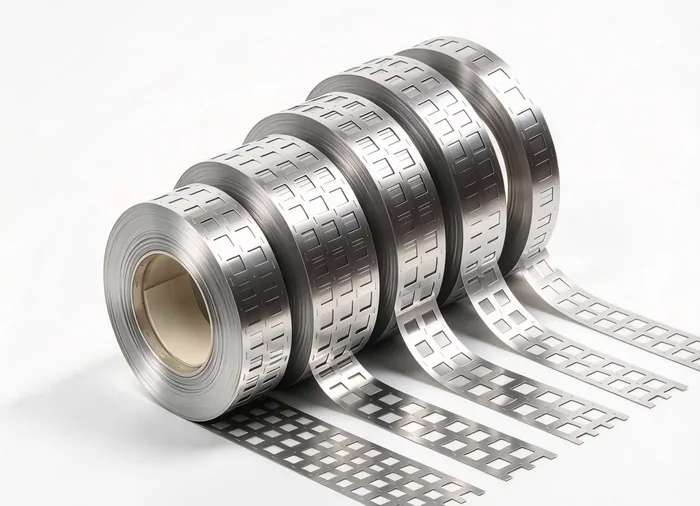
Strip and preformed rings for tube-to-tubesheet and automated joints.
Welding Monel to steel and unsure about dilution? Send the joint detail — we advise on buttering and heat input.
Ask about dissimilar joints →One classification, three delivery forms, all from the same batch route.
For K500 base metal, weld in the annealed condition and age afterwards — welding aged material risks cracking in the heat-affected zone. Send your specification — our engineers confirm availability and test values before you order.
The deposit must match the parent metal in corrosion behaviour, not only in strength. Values below are typical for the as-welded deposit and are confirmed per batch.
Porosity is the main defect risk with nickel-copper fillers; the titanium addition and a clean, dry joint are both part of the control.
As welded, typical
As welded, typical
As welded
Deposit, nominal
Recommended maximum
Monel base metal
Nickel-copper filler is sensitive to moisture pickup, which shows up as porosity in the first pass.
Rods protected until opening.
TIGStable feeding for orbital.
MIGDeposit analysis per batch.
DocumentationMoisture barrier for sea freight.
Exportto drawing for automation.
AutomationFor OEM supply.
OEMDo not preheat Monel. Preheat increases dilution and porosity risk; clean the joint and control interpass temperature instead.
Five controlled steps, each with a named output — so nothing is agreed verbally and lost between shifts.
We check grade, size, temper, tolerance, packing and delivery date against what the drawing actually needs — and flag anything the process cannot hold.
ERNiCu-7 confirmed against your existing grade number, with datasheet and typical test values issued before the order is placed.
Drawn and cleaned to a lubricant-free surface before packing.
Degreased, dried and sealed in tubes or layer-wound spools.
Chemistry, mechanical properties, dimensions and surface checked against the order, then packed for export with the documents inside the case.
Four service environments that need the Monel family end to end.
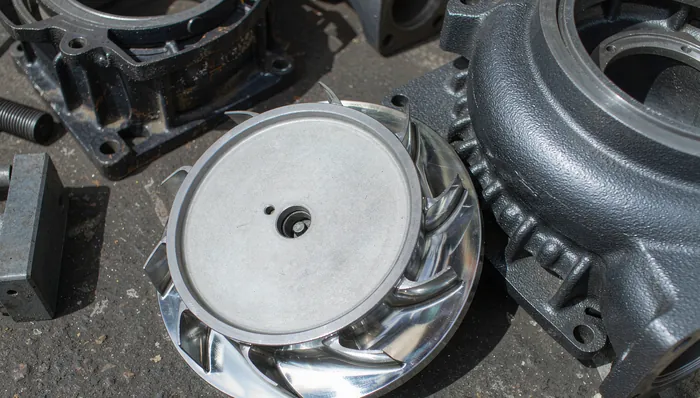
Piping, strainers and pump parts welded in Monel.
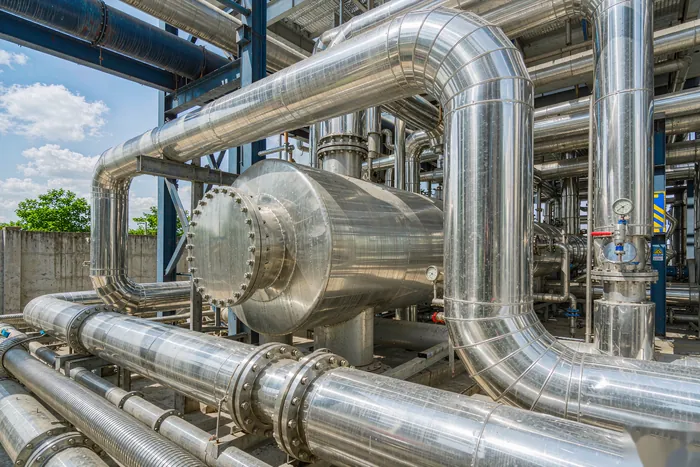
Service where nickel-copper is the specified alloy.
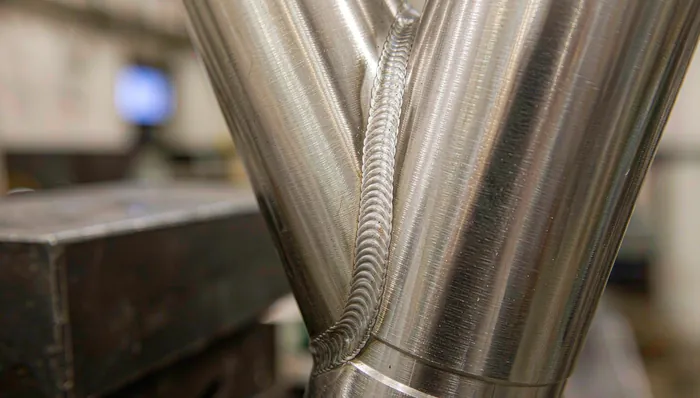
Chloride resistance without pitting at the weld toe.
Machinable, corrosion-resistant repair deposit.
A mismatched filler does not fail in the weld — it makes the parent metal corrode at the weld toe.
The correct nickel-copper filler, not a substitute.
Controlled porosity in the first pass.
Moisture pickup is the main porosity source.
Parameters that suit the alloy family.
For procedure qualification.
Trial tubes and production spools.
Each had a corrosion or porosity problem that traced back to filler or heat input.
Weld toe corrosion traced to a nickel-chromium filler used as a substitute; ERNiCu-7 restored the matching corrosion behaviour.
Parts welded in the annealed condition with ERNiCu-7, then aged to hardness, with no heat-affected zone cracking.
Machinable nickel-copper deposit for a seawater pump housing, machined back to tolerance after welding.
Tell us the base metals, thickness and service. We confirm the classification and quote rods or spools within 24 hours.
Questions about welding Monel and nickel-copper alloys.
No. A nickel-chromium filler makes the weld cathodic to Monel and the parent metal corrodes at the weld toe. Use ERNiCu-7.
No. Preheat increases dilution and porosity. Clean the joint and keep interpass below 150 °C.
Weld in the annealed condition, then age. Welding aged K500 risks heat-affected zone cracking.
Usually moisture or contamination. Keep rods sealed, clean to bright metal and use dry argon.
Yes, 1 m lengths in sealed tubes, from 1.6 to 3.2 mm.
One tube of rods or one 12.5 kg spool.